Demineralizer Systems
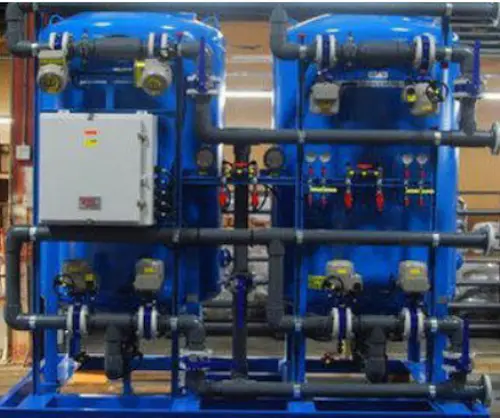
High-Purity Industrial Demineralizer Systems (DM Plants)
Industrial demineralized water is a fundamental operational requirement across high-precision manufacturing, laboratory testing, and thermal power applications. At Dubai Water Treatment, we design, manufacture, and install state-of-the-art demineralization Systems (DM Plants) engineered to completely strip dissolved mineral ions, salts, and total dissolved solids (TDS) from raw water supplies. Depending on your facility’s daily volumetric capacity, our high-purity systems utilize a sophisticated combination of advanced membrane separation technologies and specialized ion exchange resins to achieve a highly polished, zero-conductivity liquid output.
The Ion Exchange Resin Regeneration Process
The heart of an industrial Demineralizer system relies on high-capacity cation and anion exchange resins. Because these porous media beds have a finite capacity to absorb mineral ions, they eventually become saturated and require systematic chemical regeneration.
Our automated systems execute a precise, multi-stage ion exchange resin regeneration protocol, flushing the resin beds with highly controlled, concentrated solutions of hydrochloric acid (HCl) and sodium hydroxide (NaOH). This chemical flushing safely strips away trapped mineral ions and fully restores the system’s active deionization capacity. This efficient, cyclical process guarantees that your plant consistently outputs ultra-pure water with zero operational interruption.
High-Intent DM Plant Applications & Industries
Our custom-engineered dual-bed and mixed-bed demineralizers are built to meet the most stringent water quality standards across diverse, high-demand sectors in Dubai and the UAE:
- High-Pressure Boiler Feedwater: Eliminating all trace minerals to prevent devastating scaling and turbine erosion inside high-pressure thermal steam plants.
- Laboratory & Research Facilities: Providing ultra-pure, interference-free water for universities, medical testing centers, and advanced laboratories.
- Electroplating & Surface Finishing: Ensuring spotless chemical bath formulations for precise metal finishing and industrial coating lines.
- Electronics & Semiconductor Manufacturing: Meeting critical sub-micron conductivity limits required for delicate microchip component washing.
- Commercial Spotless Car Washing: Delivering mineral-free water that dries flawlessly without leaving any white calcium residue or water spots.
- Hospitals & Pharmaceutical Production: Supplying strict clinical-grade water that complies with rigorous medical sterilization and compounding regulations.